AI weld quality inspection
Catch weld defects
during welding, not after
AI‑SMART WELD checks the weld every second and corrects it on the spot.
After welding, MANU RT helps inspectors read the X‑ray film.
Prevent defects while welding.
Confirm them in X‑ray.
Welding is automated, but defects are still found only afterwards.
Each one means another X‑ray, reading, re-weld and re-inspection.
We catch problems while welding and link that record to the X‑ray.
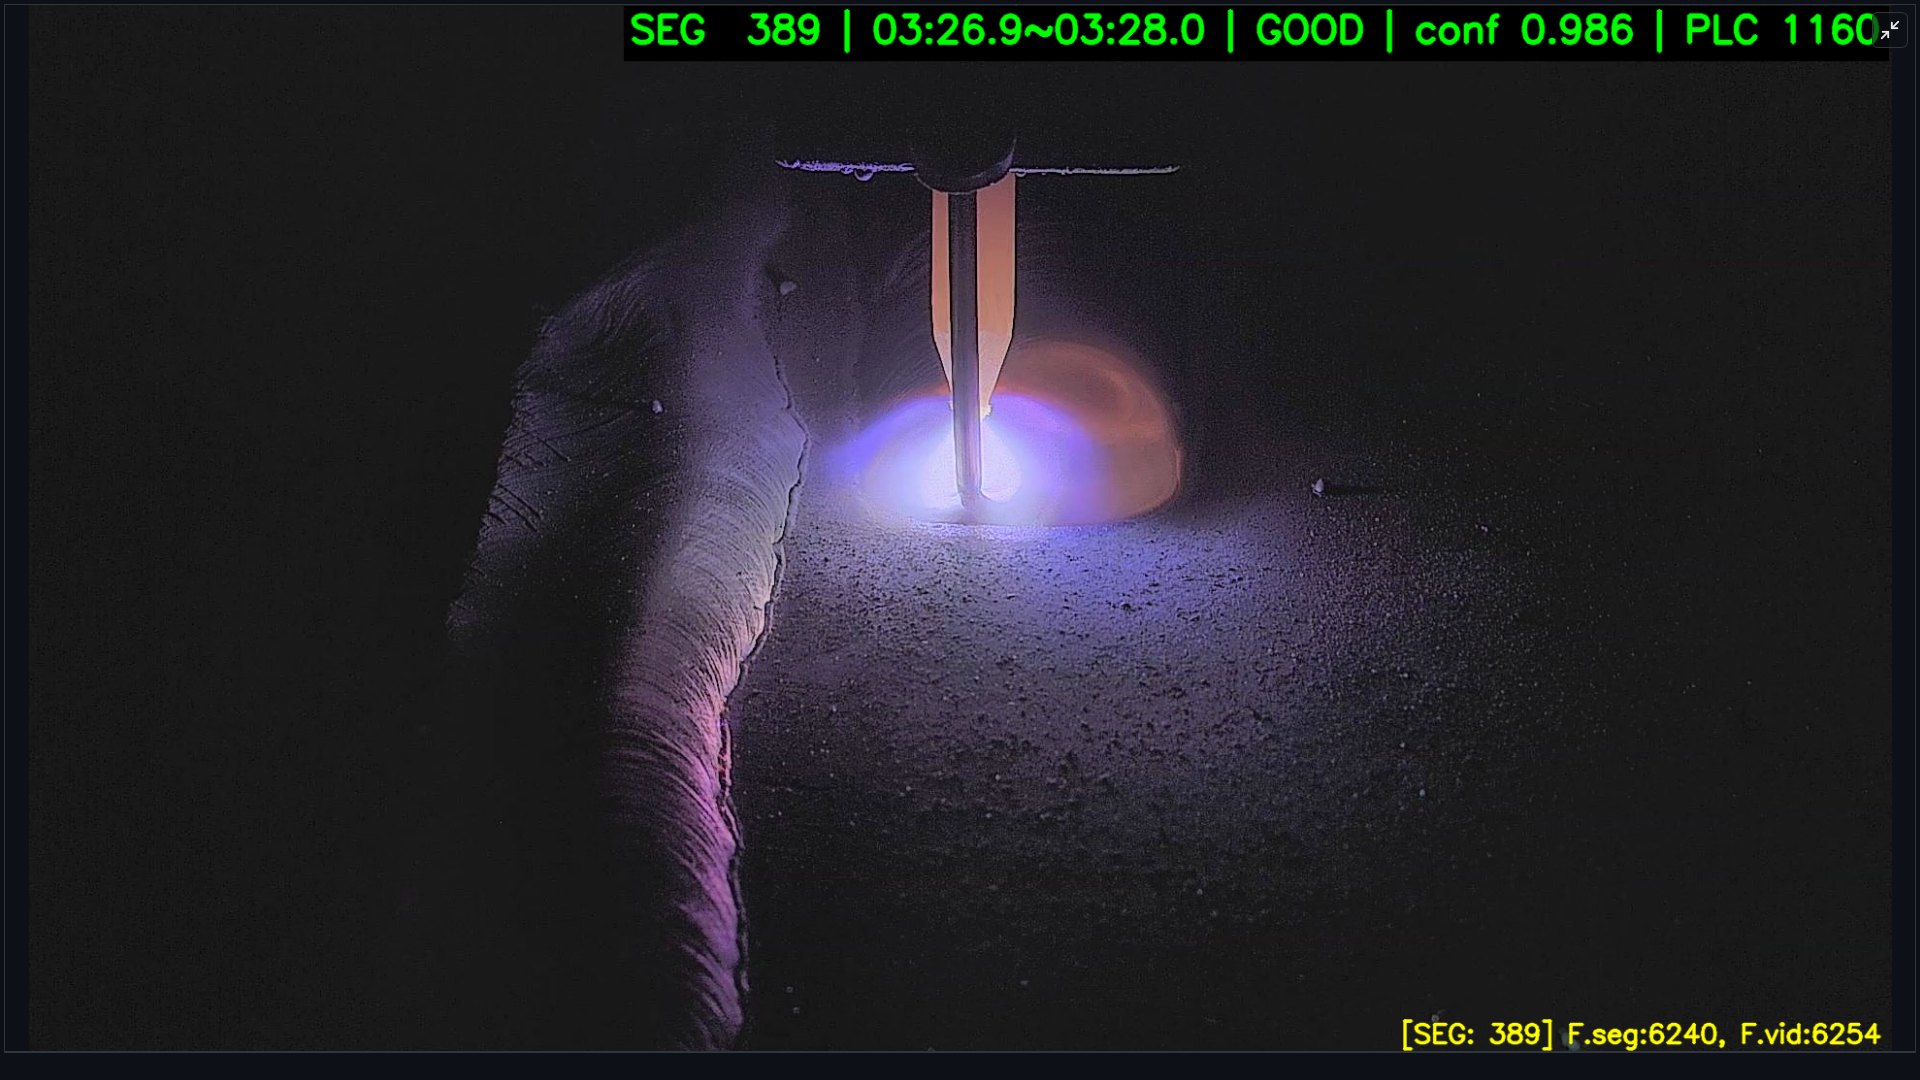
AI‑SMART WELD
In productionDuring welding- Judges weld quality about every second
- Corrects the wire feed through the PLC
- Checks the corrected weld (closed loop)
MANU RT
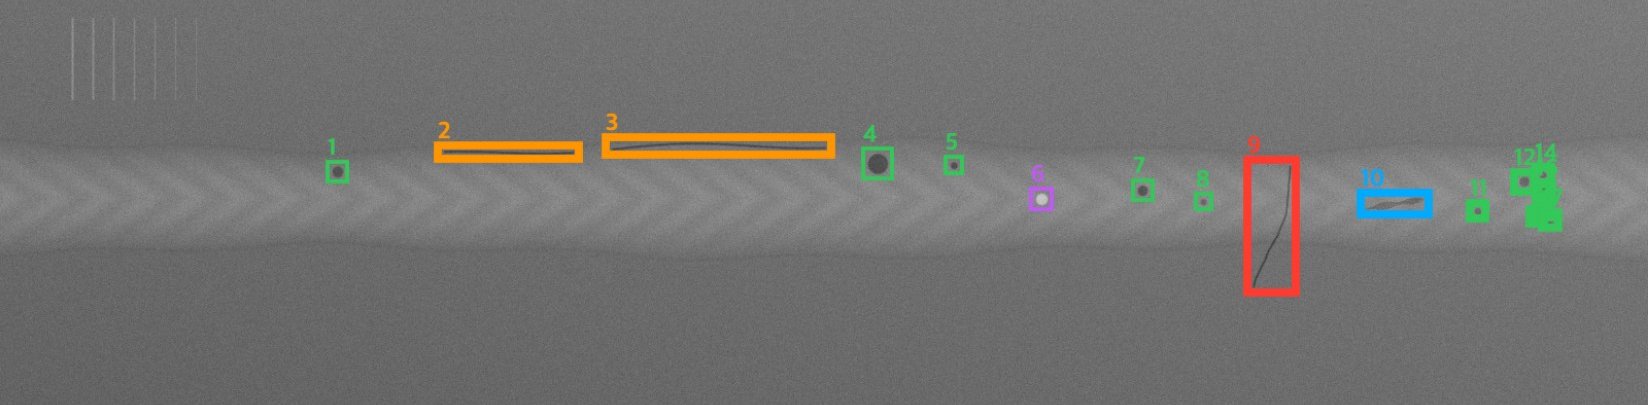
PrototypeAfter welding- Marks candidate defects on the X‑ray film
- Inspector confirms 18 defect types and signs
- Generates the X‑ray reading report
One record per seam
Welding anomalies and X‑ray defects are linked by position (mm).
Retrofit
Uses the camera and PLC already on the line.
Existing interlocks stay unchanged.
Closed loop
Corrects the wire feed every 0.5–1.0 s,
then checks the corrected weld again.
Traceable
Every segment is recorded with video,
then linked to X‑ray results by position.
7 of 12 X‑ray defects start
with welding conditions
Heat input, wire feed and travel speed cause most of what radiography finds.
AI‑SMART WELD aims to cut those defects while the weld is being made.
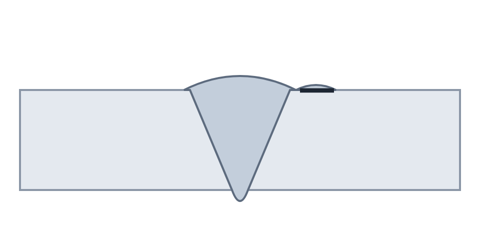
Cold lap
heat · feed · speed
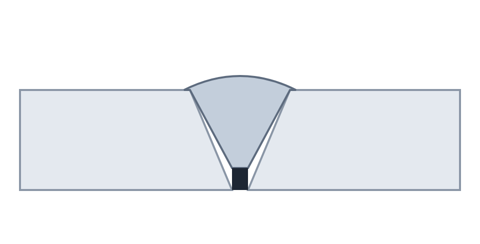
Lack of penetration
heat · feed · speed
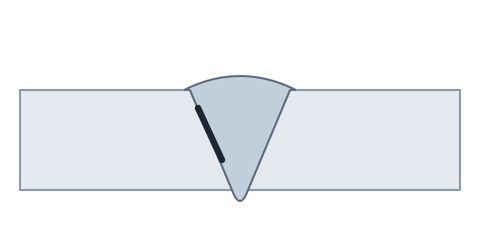
Incomplete fusion
heat · feed · speed
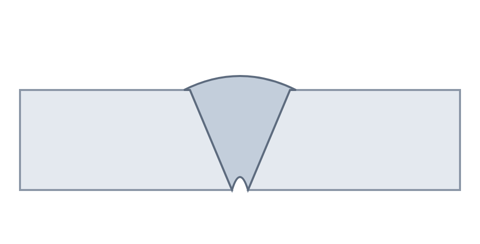
Internal concavity
heat · feed · speed
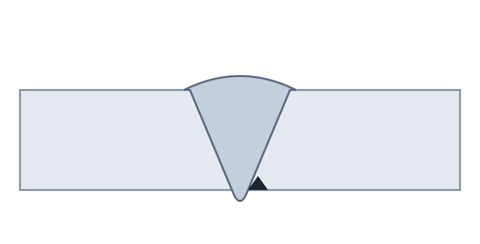
Root undercut
heat · feed · speed
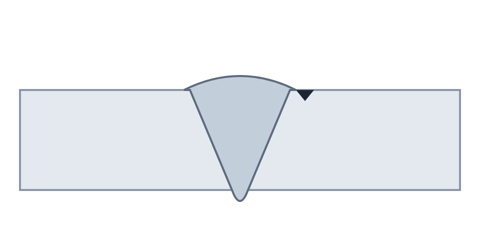
Crown undercut
heat · feed · speed
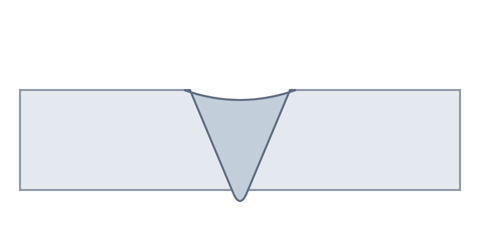
Underfill
heat · feed · speed
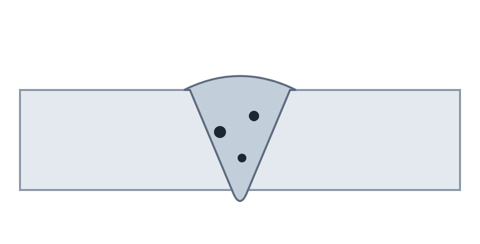
Porosity
gas · cleanliness
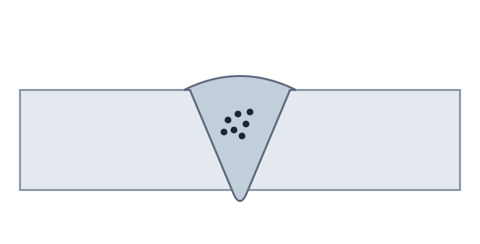
Cluster porosity
gas · cleanliness
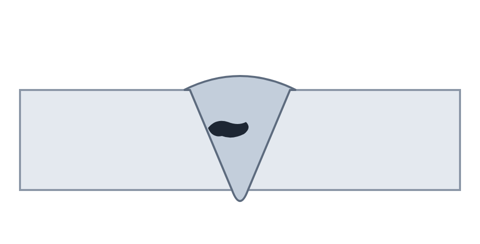
Slag inclusion
gas · cleanliness
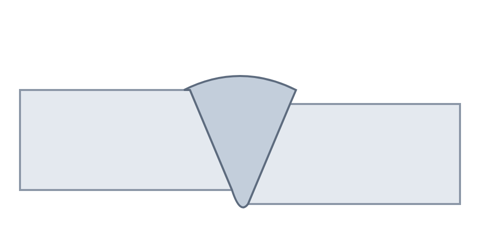
Offset
fit-up
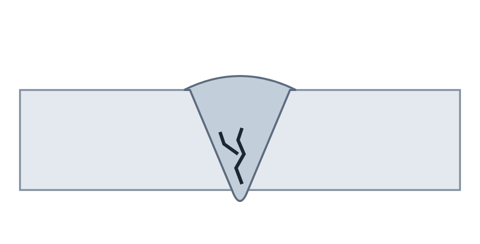
Crack
stress · material
Closed-loop weld control
01
Camera
Existing monitoring
camera on the torch02
Video converter
HDMI capture to
a digital stream03
Edge AI PC
Jetson AGX Thor
judges every second04
Operator monitor
Live verdict and
confidence on video05
PLC
LS ELECTRIC XGT gets
the new feed speed06
Wire feeder
Speeds the filler
wire up or down
Judgment
about 1 s (32 frames)
Edge PC
NVIDIA Jetson AGX Thor
PLC
LS ELECTRIC XGT
Correction
every 0.5–1.0 s
Network
offline
Records
every segment, with video
Core technologies
Video AI
Edge computing
PLC closed-loop control
Seam-position linking
X‑ray defect AI
MANU Link
MANU RT · Prototype
Welding records and X‑ray results, linked
Anomalies seen while welding are matched to X‑ray defects by position (mm).
See where, and why, each defect happened.
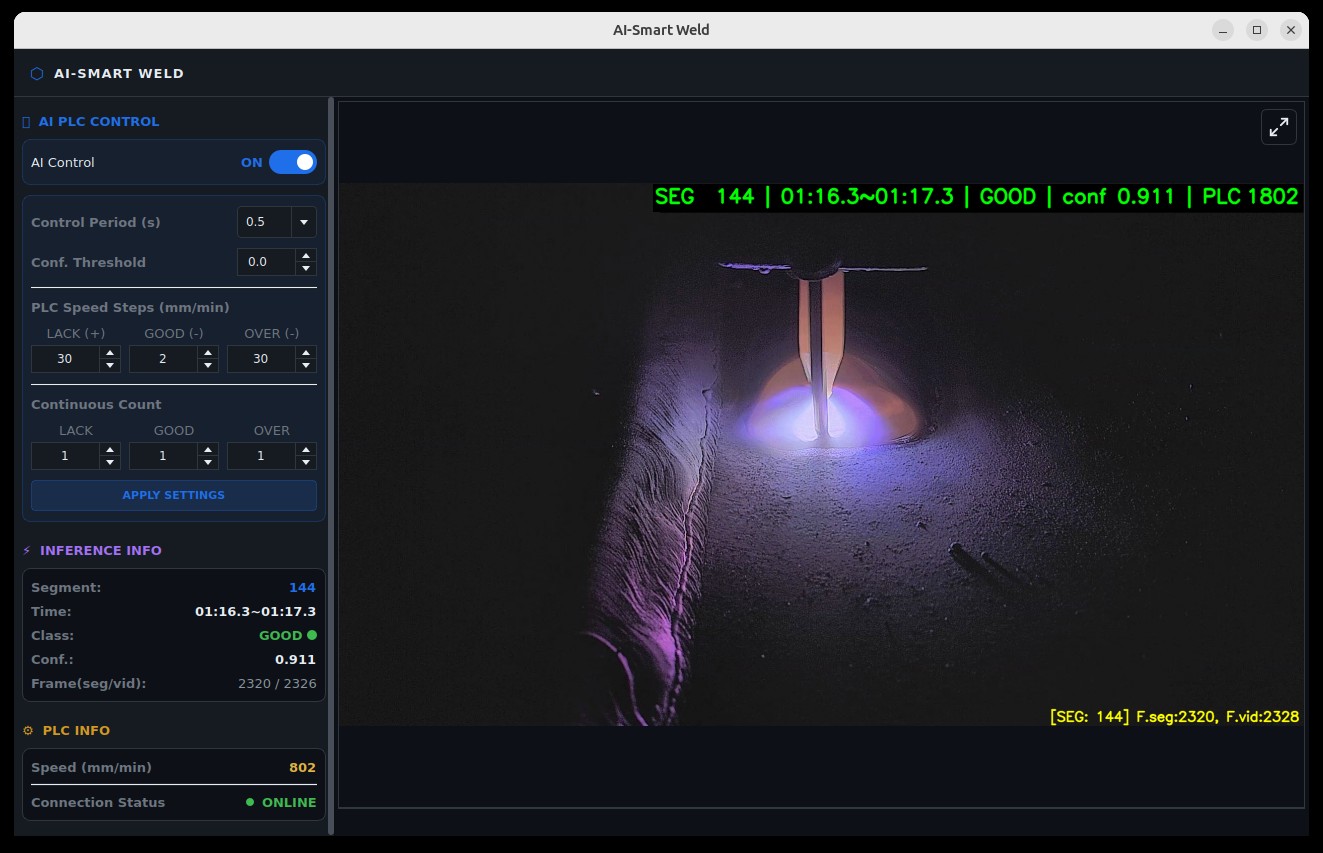
Operator software
for AI‑SMART WELD
- AI control on/off at the line
- Control period and confidence threshold
- Live inference: segment, class, confidence
- PLC speed and connection status
Proven on a production line
Results from a real welding line, checked against certified inspectors.
99.24%
AI vs. reference
verdict agreement
1,440
Weld video segments
verified
Mar 2026
In production on a
mechanized TIG line
01
Inspectors set the answer
Signed verdicts of certified inspectors
(RT Level 2 or above) are the reference.02
Every result is logged as is
The AI verdict for each defect
is recorded with no post-editing.03
Anyone can recompute it
Raw results can be shared,
so anyone can check the numbers.